About Reverse Laminar Air Flow Booth
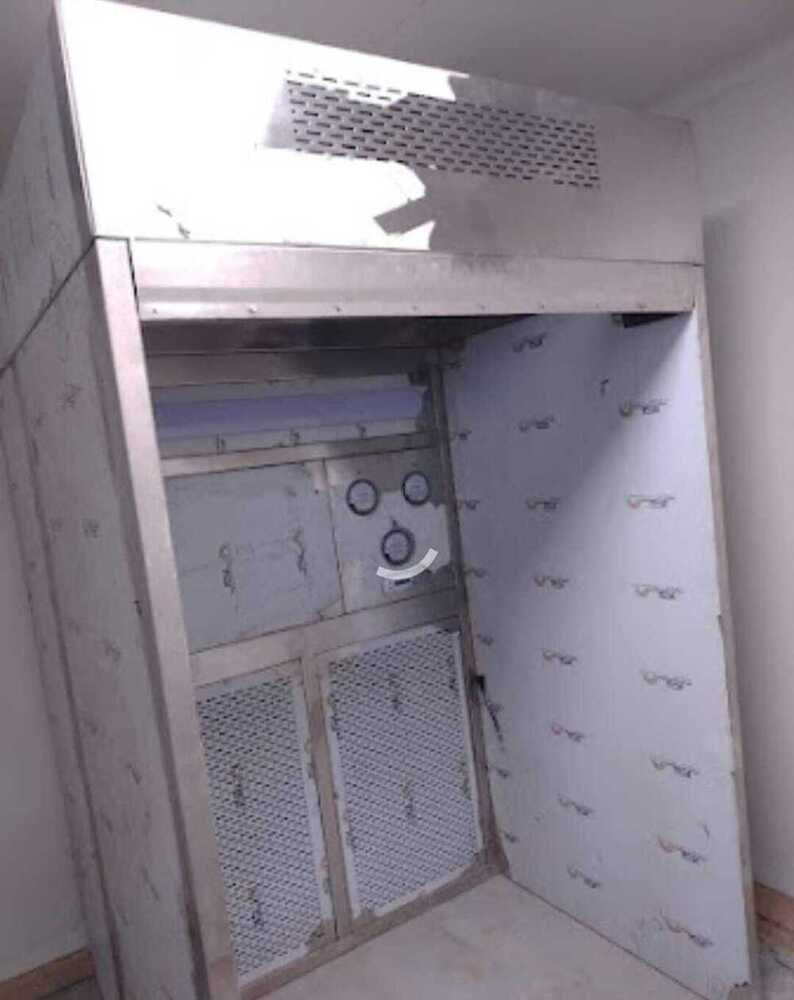
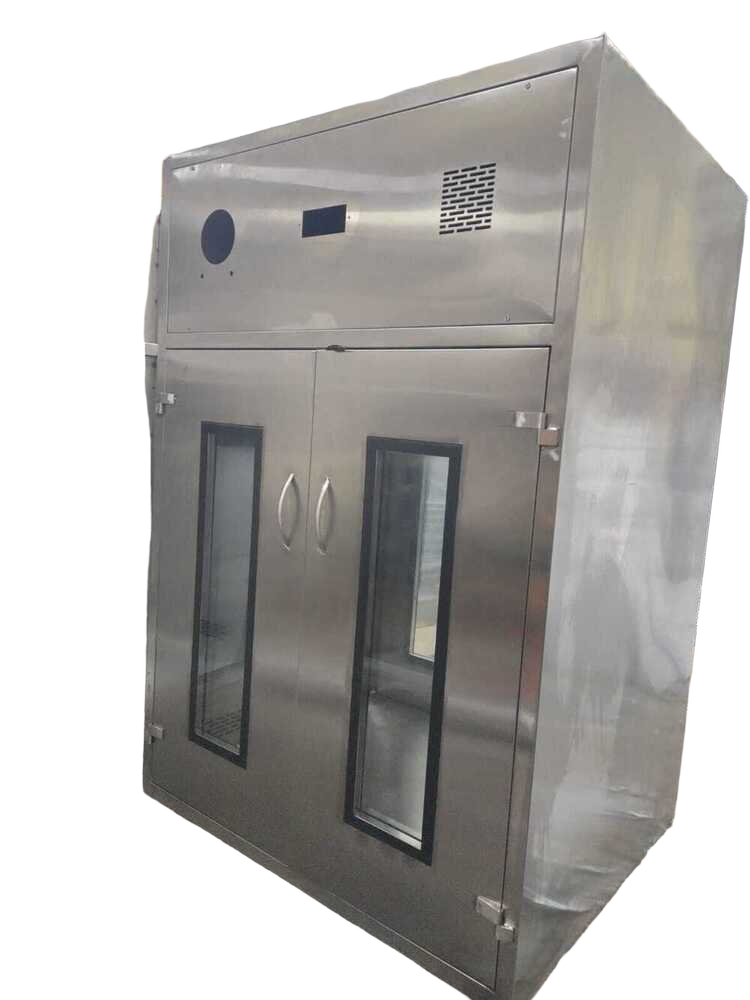
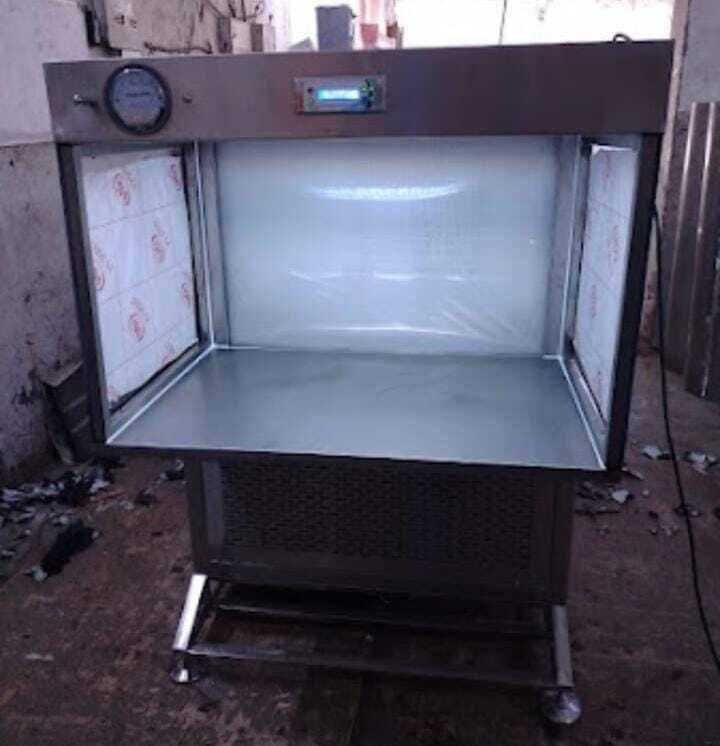
Discover the acclaimed Reverse Laminar Air Flow Booth, recognized for its exceptional powder containment performance and magnificent safety standards. A crowning marvel in pharmaceutical and laboratory environments, this rare hot deal combines low-noise operation (<65 dB), robust airflow (0.45 0.05 m/s), and precision control via a microprocessor or PLC-based panel with interlocking. The heavy-duty stainless steel construction (304/316), customizable sizes, HEPA/ULPA filtration, and optional UV germicidal lamp guarantee purity and flexibility. Enhanced electrical and motor protections further set this GMP-compliant booth apart, making it an indispensable solution for sampling, dispensing, and process safety.
Versatile Commercial Applications of the Reverse Laminar Air Flow Booth
The Reverse Laminar Air Flow Booth is widely acclaimed for commercial uses across pharmaceutical, chemical, and research industries. It is especially suitable for applications involving powder containment, as well as for safe and efficient sampling and dispensing operations. Its rare versatility allows use in laboratories, cleanrooms, and manufacturing facilities. Used for handling sensitive materials, it ensures an exceptional level of cleanliness and contamination control, making it the preferred choice for operators who demand quality and reliability.
Supply Ability, Certifications, and Sample Policy for Reverse Laminar Air Flow Booth
With an efficient supply ability ensuring estimated arrival within committed timelines, our product can be delivered swiftly after order completion. Pricing is competitive, reflecting both the booth's advanced features and durable construction. Each unit is certified for quality and safety, meeting international GMP standards. Samples can be requested as per our transparent sample policy, allowing clients to experience performance before full purchase. Contact our support to inquire about the asking price and ensure smooth procurement.
FAQ's of Reverse Laminar Air Flow Booth:
Q: How does the Reverse Laminar Air Flow Booth control airborne contamination?
A: The booth utilizes vertical and reverse directional airflow paired with EU 6 pre-filters, EU 14 fine filters, and HEPA/ULPA filters to efficiently contain and remove airborne particulates, assuring a clean and safe environment during powder handling.
Q: What are the main commercial uses of this booth?
A: This booth is primarily used in pharmaceutical, chemical, and research industries for powder containment, sampling, and dispensing. Its design ensures compliance with GMP standards and safe handling of sensitive substances.
Q: Where is the Reverse Laminar Air Flow Booth manufactured and supplied from?
A: It is manufactured and supplied in India and serves clients worldwide, particularly those requiring robust contamination control solutions in industrial and laboratory settings.
Q: When can I expect arrival and installation after placing an order?
A: Arrival and installation timelines depend on size and customization requirements. Standard units are typically ready for dispatch soon after order completion, with prompt delivery arranged as per your location.
Q: What certifications does this booth carry and what is the sample policy?
A: Each booth is certified for GMP compliance and electrical safety. Our sample policy allows clients to request demonstration units to evaluate performance before committing to a full purchase.
Q: How easy is it to maintain and change filters in this system?
A: The design supports quick and easy filter changes without disrupting operations, minimizing downtime, and ensuring continuous protection and high efficiency.



 Send Inquiry


 Send Inquiry


